01 / CONTINUOUS HEATING
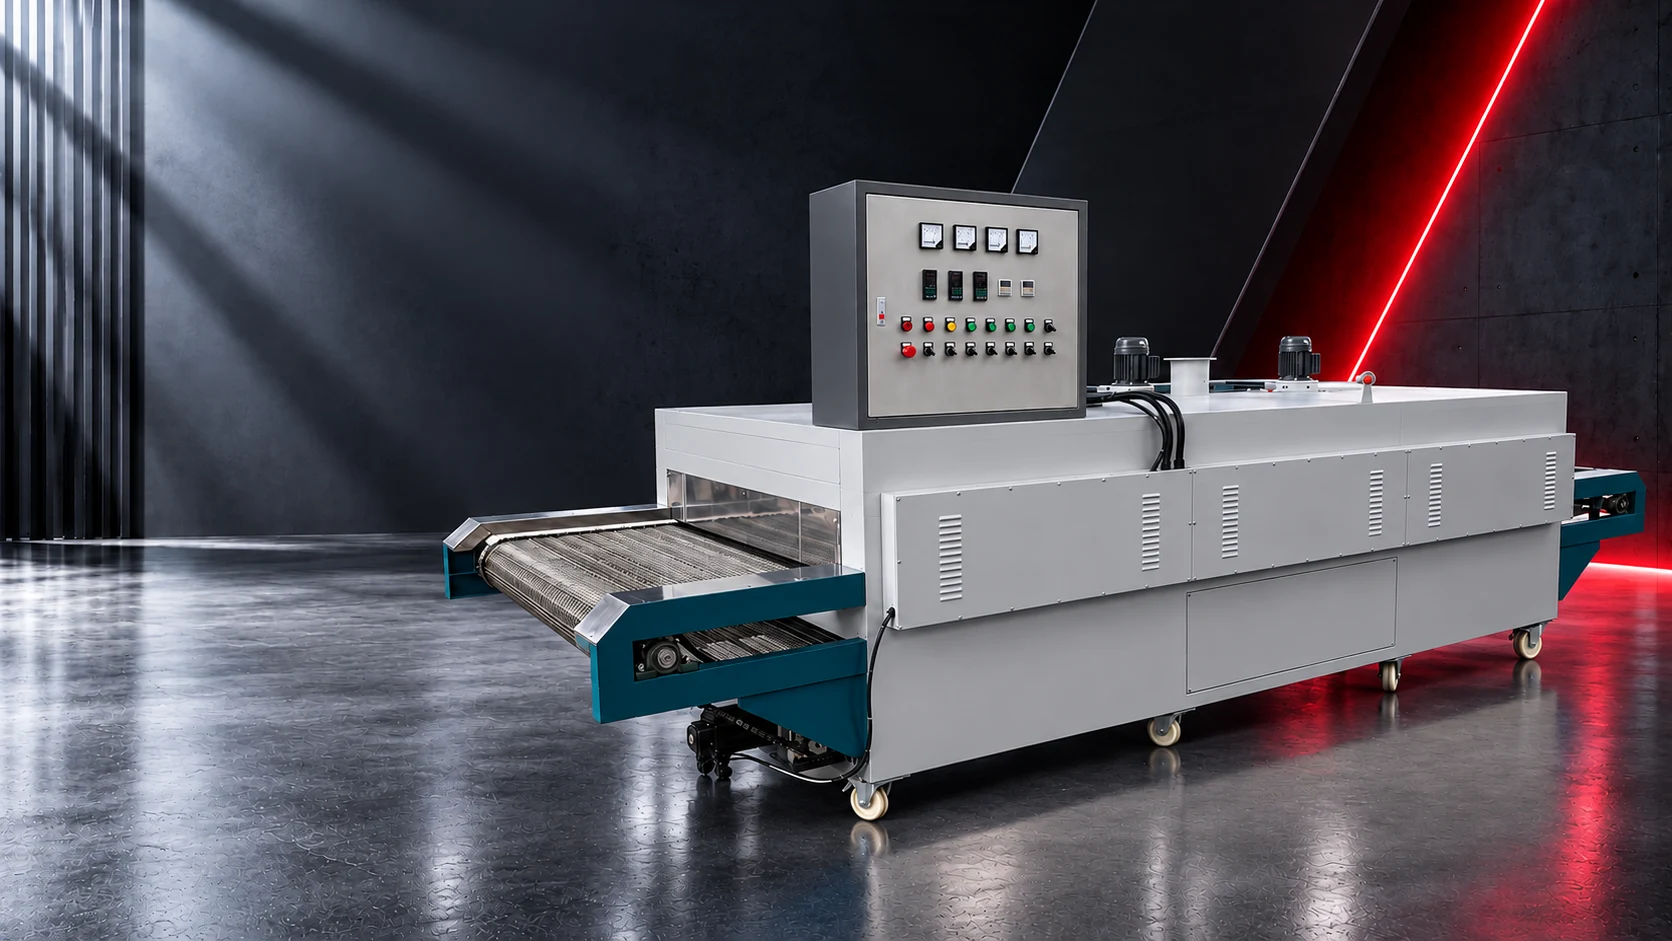
Wire-mesh conveyor ovens
A metal mesh belt carries the load continuously. Check part size, mesh openings, load support and airflow needs before setting belt width and spacing.
Send conveyor requirements ↗ DIANREZHANELECTRIC HEATINGGet a preliminary selection ↘
CONVEYOR OVENS / CONTINUOUS PROCESSING
Match the line speed
to the process.
Compare wire-mesh, flat-belt and roller conveyors for continuous preheating, drying and curing. Start with part dimensions, hourly throughput and the required temperature profile, then match heated length, speed and loading.
01 / EQUIPMENT ARRANGEMENTS
A metal mesh belt carries the load continuously. Check part size, mesh openings, load support and airflow needs before setting belt width and spacing.
Send conveyor requirements ↗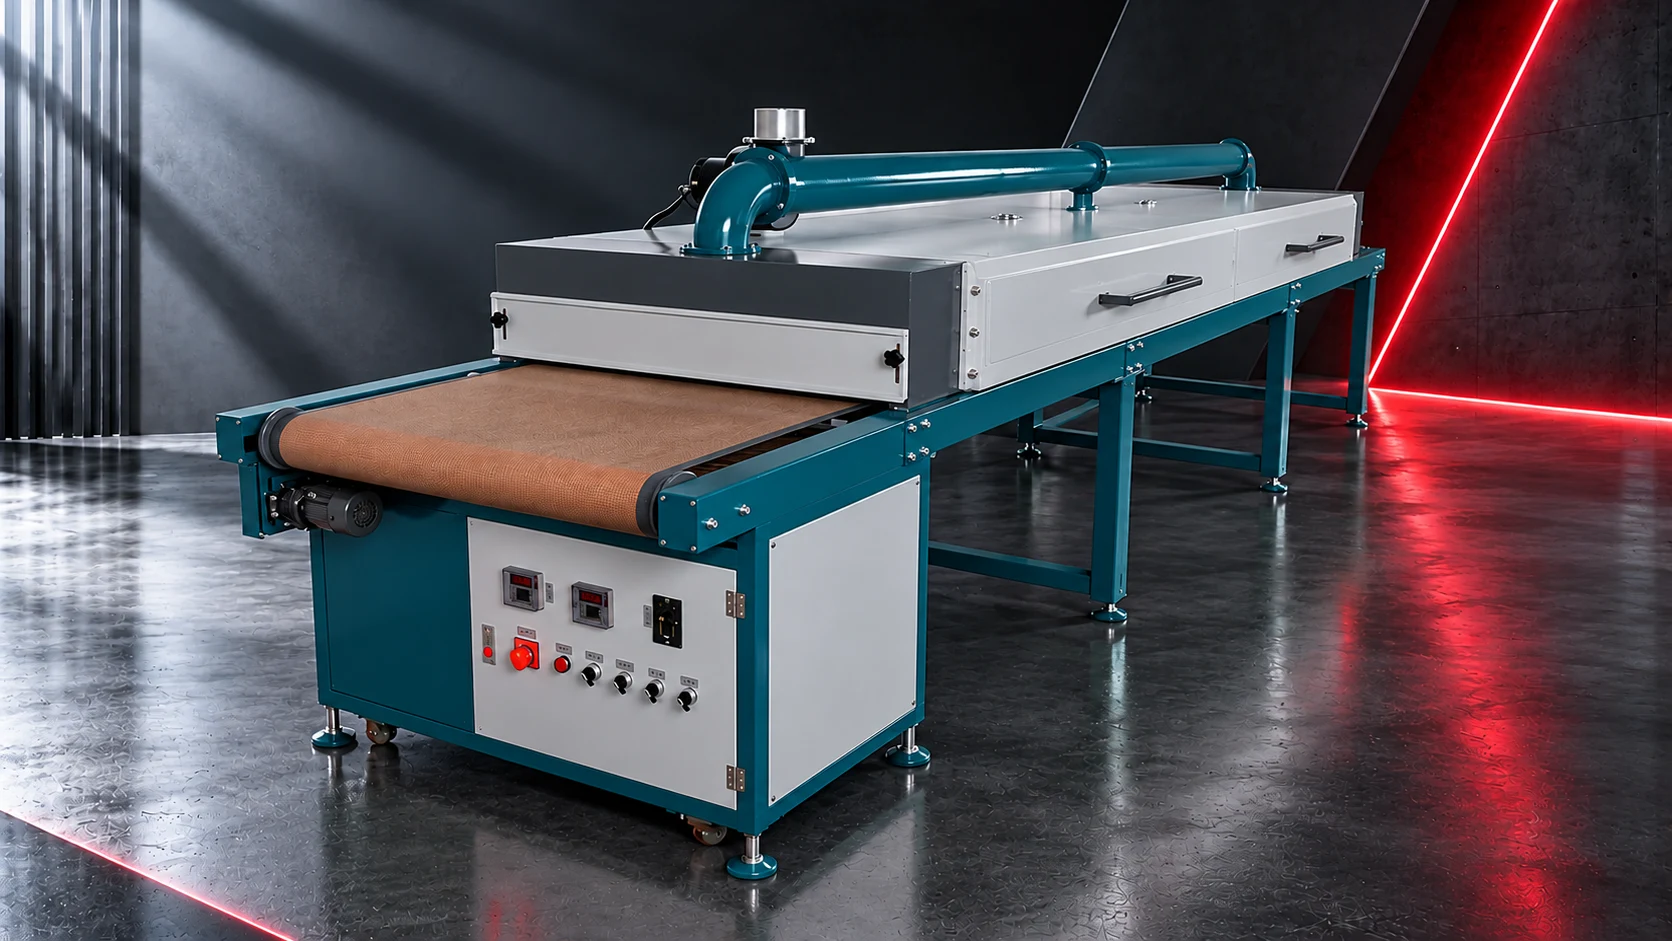
A continuous flat belt supports the product. Confirm belt material suitability, process temperature, contact requirements, tracking and cleaning access.
Send conveyor requirements ↗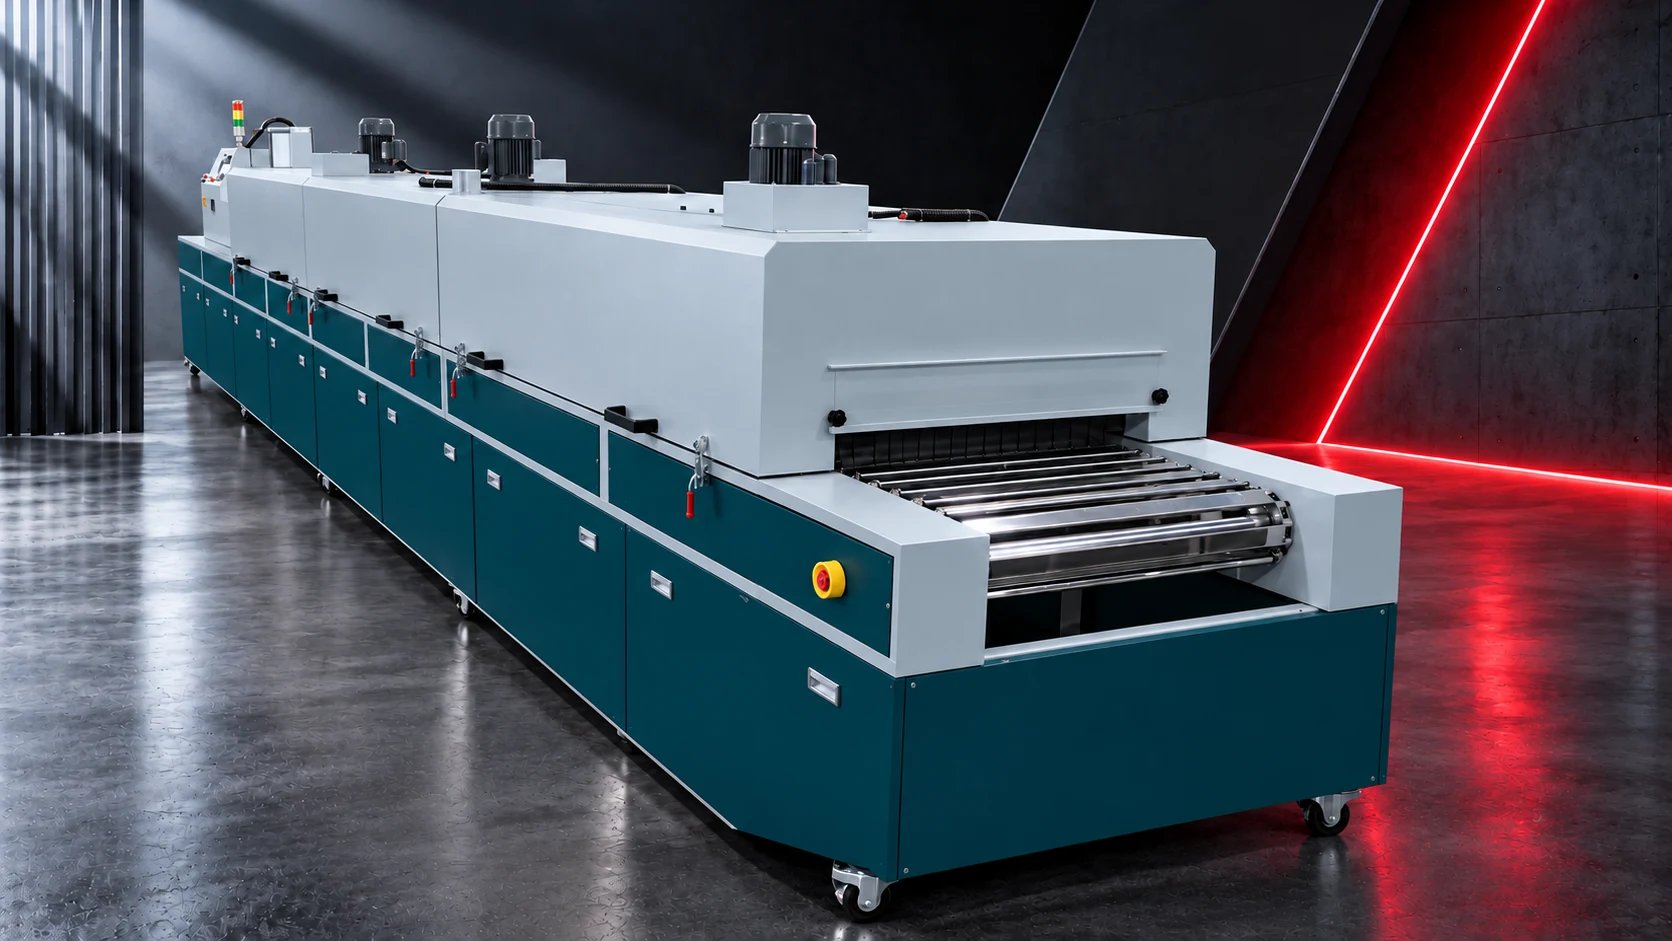
Rollers carry rigid parts or trays through the line. Check the underside, roller pitch, supported length, load and upstream and downstream transfer.
Send conveyor requirements ↗Renders are based on supplied equipment photographs and illustrate conveyor arrangements. Heating method, zone count, dimensions and load capacity depend on the confirmed process.
STRUCTURE COMPARISON
A mesh belt, flat belt and roller bed have different support and cleaning requirements. Confirm the product base, carrier and process substances before choosing the transport system.
Swipe the table sideways on smaller screens.
| Transport | Product/support conditions | Checks | Selection limits |
|---|---|---|---|
| Wire mesh | Parts or trays that suit mesh support and through-flow | Mesh opening, load, tracking, cleaning and contact marks | Check trays for small or soft parts and possible surface marking |
| Flat belt | Parts or carriers needing continuous support | Belt temperature rating, chemical compatibility, splice and cleaning | Confirm actual belt-contact temperature and process substances, not just chamber setpoint |
| Rollers | Flat-bottom parts or trays that can span the roller pitch | Pitch, load, synchronization and transfers | Small or flexible parts may need carriers; outside dimensions alone are insufficient |
INTERACTIVE EXPLORER
Explore a mesh-belt arrangement with its supports, hood, conceptual zones and circulation equipment. Open the cutaway, change the demonstration speed and inspect interlock responses.
Conceptual model based on the product arrangement; internal geometry and flow are illustrative, not measured construction or a temperature calculation.
CONTROL & PROTECTION
A continuous line needs a defined response for products already inside the heated section as well as upstream and downstream equipment.
Define speed feedback, blockage or drive-fault detection, heat inhibition on a stop, and handling of products remaining in the hot zone.
Check their permissives separately. A command to run a fan is not proof of airflow. Solvent release needs its own assessment.
Review zone sensors, independent high-limit cut-offs and alarm records. Define air temperature, product temperature and protective limits separately.
Specify responses to emergency stop, power loss and downstream stops, including recovery conditions. Fan, conveyor and heater sequences depend on the equipment design.
Design principles: Grieve · General oven instructions · Despatch · Engineering guide
02 / SELECTION CHECKS
Part dimensions, mass, underside and tray or fixture details determine support and clearance requirements.
Specify parts or mass per hour, lane count, product spacing and upstream and downstream cycle times.
Separate air setpoints from required part temperatures. State the criteria for heat-up, soak, drying or curing.
Residence time = heated path length ÷ conveyor speed. This is travel time through the heated path, not necessarily soak time after the part reaches temperature.
Review heating zones, circulation, moisture and volatile release against the process. Appearance alone does not establish the heating method or hazardous-process suitability.
Confirm loading height, total footprint, utilities, cooling sections, service clearance and interfaces to adjacent equipment.
03 / PROCESS SEQUENCE
Set product spacing, lane count and carrier arrangement for stable loading.
Arrange the heating sections around the required part temperature profile.
Validate drying, curing or soak requirements against line speed and heated path.
Match cooling, unloading and the next operation to the product temperature limit.
04 / PRACTICAL QUESTIONS
Start with stable product support, temperature and contact requirements. Check mesh openings against part size, flat-belt material against the process, and roller pitch against the product underside. Slat, chain and dedicated-carrier arrangements can also be reviewed for other loads.
A higher speed reduces residence time in a fixed heated path. Validate the part temperature profile and process result before changing speed, while also checking product spacing, lane count and adjacent line capacity.
No. The installed length may also include loading and discharge extensions, transitions, cooling and drive sections. Specify the heated path separately from the overall installation footprint.
Not necessarily. Use the required part temperature, moisture level, cure result or other acceptance criterion. Air temperature and residence time are process inputs, not substitutes for product acceptance.
Manufacturer guidance provides further context on conveyor arrangements and preliminary oven length planning.
Grieve · Conveyor oven length ↗Wisconsin Oven · Conveyor ovens ↗Convert speed, residence time and heated travel length before discussing the layout.
Open process calculator →05 / YOUR PROCESS
Start with the product, output and process time. Add any known belt speed, temperature profile or site constraints, then provide contact details to send your requirements.